Step 02.03 — Re-check the iron with the LDO tip on the first insert
Step 3 of 44 · Chapter 02 — Z drives, Z idlers, Z rails, deck panel
Tap to enlarge
Parts:
- M3×5×4 brass heat-set insert ×1 · Fasteners, Tools & Misc box
-
z_drive_retainer_a×1 · bin 02-Z0, 02-Z2 - soldering iron with the LDO brass tip · tool
Do:
- Heat the iron to the temperature taped on it at Gate B.
- Drive one insert 90 % into the Gate B retainer, then press it flat with a steel block.
- Let it cool and inspect it.
Check
The insert went in square in under 5 seconds, sits flush to 0.2 mm proud, and its boss has not bulged.
What you're looking at
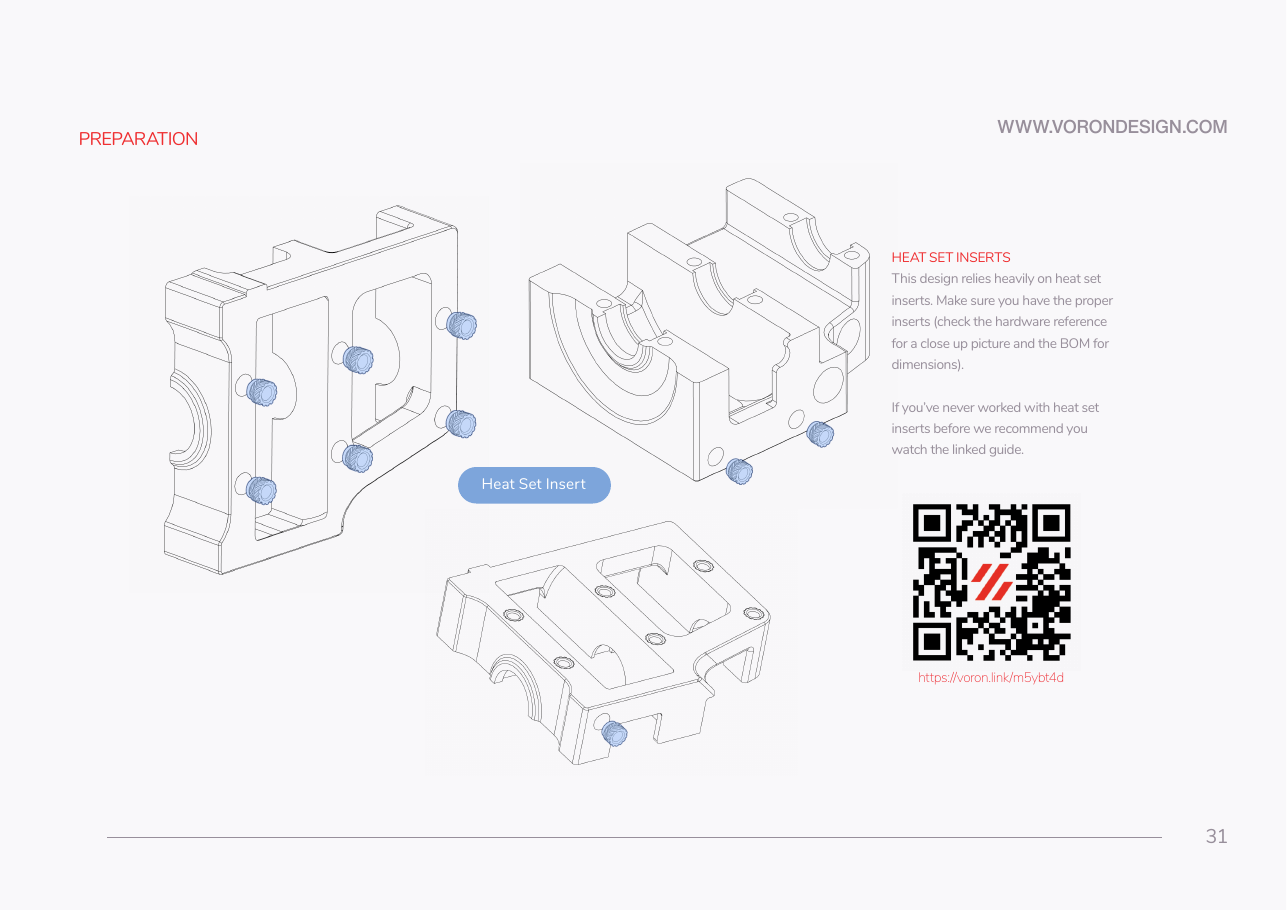
Manual p.31: the blue pills are inserts going into Z-drive bosses. Gate B found the iron temperature with the stock conical tip and filled the Heatset_Practice coupon. The LDO tip is different brass, so the first real insert re-checks that number. See the glossary.
Caution
Rev D+ / LDO: the kit supplies the brass tip and 153 inserts for the whole build; this one is the first of the 36 in the drive parts, and none go into a coupon. A bulge means 10 °C cooler and a slower push before the next insert, and a reprinted retainer. src
Caution
Iron back in its stand between inserts, bench ventilated. The tip and a freshly set insert both burn: hold parts by the far edge until they cool.
Tip
Do not leave the iron sitting in a part, or powered longer than needed: the brass tip oxidises.
Source: Voron manual p.31 · LDO heat-set insert tool guide · LDO 350 Rev D BOM