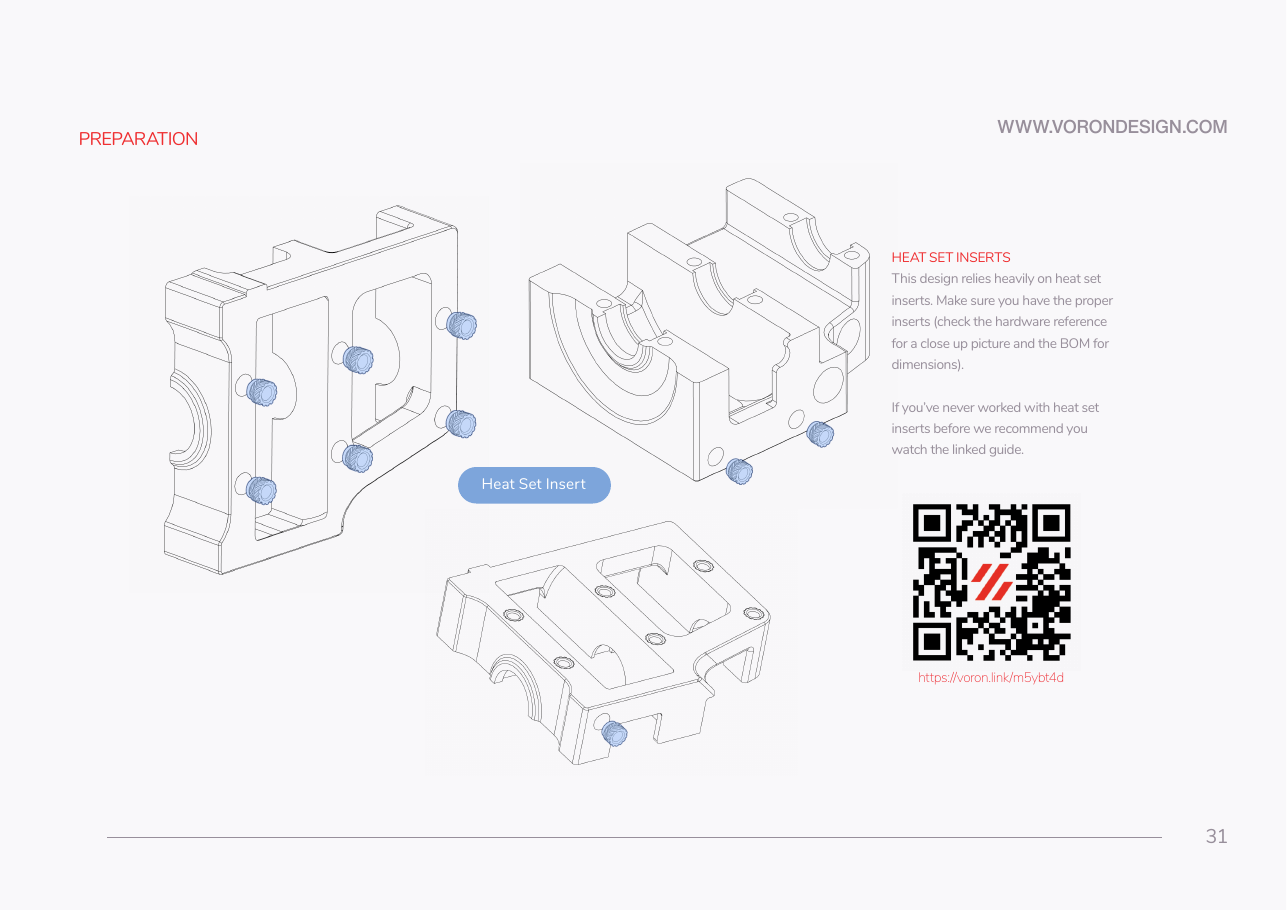
Step 02.04 — Seat the heat-set inserts in the Z drive parts
Step 4 of 44 · Chapter 02 — Z drives, Z idlers, Z rails, deck panel
Tap to enlarge
Parts:
- M3×5×4 brass heat-set insert ×35 · Fasteners, Tools & Misc box
-
z_drive_retainer_a×1 · bin 02-Z0, 02-Z2 -
z_drive_retainer_b×2 · bin 02-Z1, 02-Z3 -
z_drive_main_a×2 · bin 02-Z0, 02-Z2 -
z_drive_main_b×2 · bin 02-Z1, 02-Z3 - the Gate B retainer with its first insert · already on the bench
Do:
- Seat 7 inserts per
z_drive_retainerand 2 perz_drive_main, flush; the Gate B retainer takes 6 more. Let each part cool. - Insert pockets are Ø4.7 × 5 mm deep. Ø6 counterbores on the main's flat face take no insert.
Check
36 inserts in, every one flush or a hair below, none cocked, no melted bulge, nothing in a counterbore.
What you're looking at
In front of you are the four retainers and four drive mains. The thirty-six inserts are the threads that hold each drive closed: the six in each retainer's flat face take the M3×40s, the three in the drive's foot face take the baseplate's M3×8s.
Caution
Iron back in its stand between inserts, bench ventilated. The tip and a freshly set insert both burn: hold parts by the far edge until they cool.
Tip
The retainer's 7 are 6 in the flat print face plus 1 in a side face; the main's 2 are both in one side face.
Tip
Count the Ø4.7 pockets on your own parts before you start; if a part shows a different number, trust the part. A plain M3 clearance hole is Ø3.4 mm.
Good stopping point · ~40 min since the last one
printed parts sorted into a and b piles and inspected, the iron temperature confirmed on the coupon, and all 36 heat-set inserts seated in the four retainers and four drive mains. Unplug the iron. Nothing is assembled.